Visionary Knowledge
Lamination: The Overlooked Process That Can Make or Break Your Graphics
Published Date: November 2026

Visionary Knowledge
Published Date: November 2026
You profile your printer for different media. Why aren’t you profiling your laminator for different laminates?
In the wide-format printing industry, we invest considerable time and effort into achieving the best possible print quality. We carefully select our media, calibrate our printers and create individual print profiles to ensure consistent results.
But what happens when that perfectly printed graphic reaches the laminator?
For many print businesses, the answer is surprisingly simple: they use essentially the same laminator settings regardless of the film being applied.
And that’s where problems can begin.
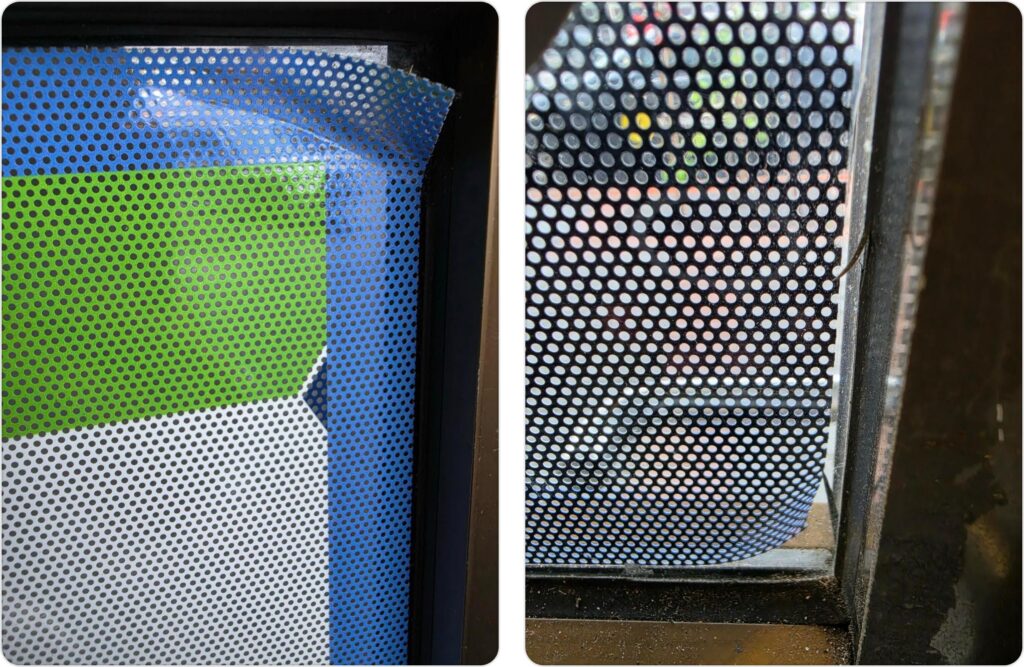
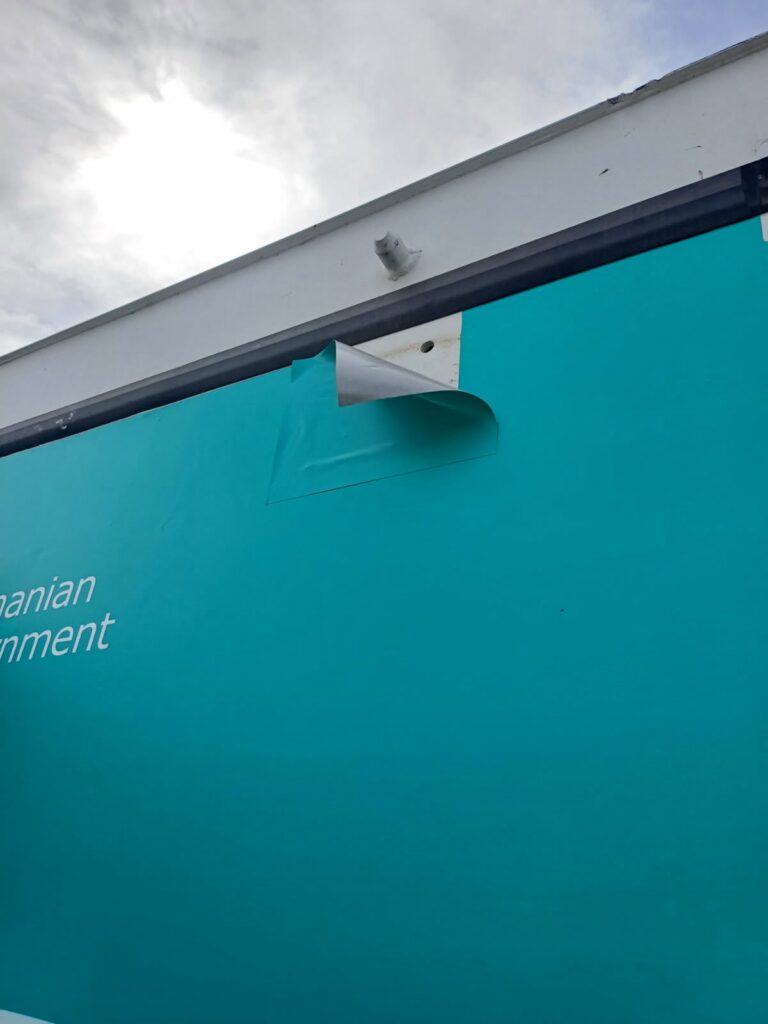
At Visionary Digital, we regularly hear from customers experiencing issues with laminated graphics lifting, curling or pulling away from surfaces after installation. These problems are particularly noticeable with one-way vision films, but they can also occur with conventional self-adhesive vinyl (SAV).
Naturally, when a graphic begins lifting, the first suspicion often falls on the adhesive or the media itself. However, in our experience, the problem frequently originates not with the printed film but with how the laminate was applied.
Understanding why this happens can help printers avoid expensive reprints, installation failures and unnecessary material waste.
One of the most common causes of laminated graphics lifting is excessive tension during lamination. When a laminate is applied under too much tension, the film can stretch as it passes through the laminator.
Initially, everything may look perfectly fine. The finished graphic appears flat, the laminate is securely bonded and there are no obvious signs of a problem.
However, many films have a natural tendency to recover towards their original dimensions after being stretched. This is often referred to as film memory or elastic recovery.
Once the graphic has been installed, the stretched laminate may begin contracting. Because it is bonded to the printed film underneath, that contraction creates stress across the entire construction. The result can be:
With one-way vision films, the problem can be particularly pronounced because the perforated construction provides less continuous material to resist the forces generated by the laminate.
The important point is that even an excellent adhesive cannot always overcome the mechanical stress introduced by an incorrectly applied laminate. This is why controlling laminate tension is so important.
Here’s where things become interesting. A 30-micron laminate behaves very differently from a 200-micron laminate.
Likewise, a cast PVC film behaves differently from a polypropylene (PP) film, a polyester (PET) film or a conventional calendared PVC laminate. These materials have different physical characteristics, including:
A thin, flexible cast laminate may require a different machine setup from a relatively stiff 200-micron film. Similarly, a polypropylene laminate may behave differently under tension and temperature compared with a PVC laminate.
Even two laminates of similar thickness can require different settings because of their construction and adhesive systems.
So why would we expect one set of laminator settings to deliver optimal results across every product? The answer is that we shouldn’t.
Consider what happens when a printer introduces a new SAV or perforated film into production. Typically, the operator will select or develop an appropriate media profile, adjusting parameters such as ink limits, curing temperatures, print speed and colour management. These settings are saved so the same results can be reproduced consistently.
Yet when it comes to lamination, many businesses rely on a familiar combination of roller pressure, tension, speed and temperature that has worked reasonably well in the past. The problem is that what works for one laminate may be entirely unsuitable for another.
At Visionary Digital, we believe lamination should be treated as a controlled production process, just like printing. That means establishing and recording a dedicated lamination profile for each laminate, taking into account the printed media being laminated.
A practical lamination profile might include:
| Parameter | What to Record |
|---|---|
| Laminate | Product name, construction and thickness |
| Print media | SAV or perforated film being laminated |
| Web tension | Unwind and rewind settings |
| Roller pressure | Nip pressure or roller gap |
| Lamination speed | Operating speed |
| Temperature | Roller temperature, where applicable |
| Film alignment | Tracking and web alignment |
| Results | Observations, issues and approved settings |
Once an appropriate profile has been established, operators can return to those settings whenever the same material combination is used. This approach removes much of the guesswork and reduces the likelihood of inconsistent results between operators, production shifts and material changes.
It also provides a valuable reference when troubleshooting problems.
As a starting principle, pressure-sensitive laminates should generally be applied with the minimum web tension necessary to maintain smooth, controlled feeding. The objective is to keep the laminate flat and free from wrinkles without stretching it.
This doesn’t necessarily mean every laminate should be run with absolutely zero machine tension. Different films and laminators require different levels of web control.
Some laminates may need a small amount of tension to maintain alignment and prevent wrinkling, while others may perform best with almost no resistance from the unwind system. The key is to distinguish between enough tension to control the film and excessive tension that stretches it.
Operators should also pay attention to rewind tension, particularly where completed graphics are wound onto a take-up roll. Excessive rewind tension can introduce additional stress into the finished construction.
The correct settings should be established through controlled testing and recorded for future use.
Heat is another important variable that deserves careful consideration. Some laminators feature heated rollers, and operators may use warmth to improve the appearance or handling of certain laminates.
Moderate heat can help some pressure-sensitive adhesive systems wet out against the printed surface, potentially improving initial contact and reducing visible silvering.
However, heat is not a universal solution. Different laminate constructions respond differently to temperature. Excessive heat may soften or distort certain films, affect their dimensions or introduce additional stress as the material cools. Heat can also influence the behaviour of the printed media underneath.
For this reason, the use of heated rollers should always be based on the laminate manufacturer’s recommendations and the compatibility of the complete media construction. A heated laminator should not be used to compensate for excessive web tension or an incompatible laminate.
Where heat is recommended, temperature should become another recorded parameter within the lamination profile. For materials intended for cold lamination, introducing heat without appropriate testing may create more problems than it solves.
Wide-format printers represent a significant investment. Businesses spend considerable money on advanced printing technology to achieve excellent colour reproduction, productivity and image quality.
Yet the laminator, which can ultimately determine whether that printed graphic performs successfully in the field, is sometimes treated as a secondary consideration.
A good laminator needs to do much more than simply press two films together. It should provide consistent and controllable web tension, uniform roller pressure, accurate tracking and reliable operation across different material constructions. The ability to make precise, repeatable adjustments is particularly important when working with thin or sensitive laminates.
This doesn’t mean every print business needs the most expensive laminator available. It does mean that laminator quality, maintenance and operator training deserve the same attention as the printing process itself.
A perfectly printed graphic can still become an expensive failure if the lamination process introduces unnecessary stress.
One-way vision films present some unique challenges. Unlike conventional SAV, a perforated film contains thousands of small holes, reducing the continuous surface area of the material.
When a solid laminate is applied over this perforated structure, the laminate and printed film become a combined construction with different mechanical characteristics. If the laminate has been stretched during application, its recovery forces can place additional stress on the perforated film and its adhesive bond to the installation surface. This can contribute to edge lifting, curling and other installation problems.
For this reason, selecting a laminate specifically suitable for perforated window graphics is important. However, even the correct laminate can perform poorly if it is applied under excessive tension. The choice of laminate and the way it is applied are equally important.
The financial impact of a failed graphic extends well beyond the cost of the material. There is the time spent investigating the problem, reprinting and laminating replacement graphics, organising installers and potentially returning to site. There is also the less visible cost of interrupted production schedules and customer dissatisfaction.
Many of these problems can be avoided through better process control. By treating lamination with the same discipline as printing, businesses can improve consistency, reduce waste and minimise the risk of installation failures.
At Visionary Digital, we work closely with printers and installers to understand how our materials perform in real-world applications. One of the most valuable lessons we’ve learned is that the performance of a finished graphic depends on more than the quality of the materials. It depends on how those materials are processed.
The next time you change laminates, consider whether your laminator settings should change too.
After all, if you wouldn’t use the same print profile for every media, why would you use the same lamination settings for every laminate?
Visionary Digital | Technical Insights
Helping Australian wide-format printers achieve better results through smarter material selection, application techniques and production practices.
3 July 2026

On a project like the 100 St Georges Terrace renovation, there’s no room for materials that don’t hold up. So when Discus Print & Signage chose to build the site hoarding from Gboard, finished with Visionary’s PVC-free self-adhesive vinyl, it was a real test of whether sustainable materials could do the job — and do it better.
We spoke with Steve Filear, General Manager of Discus, to talk through the project and why more of the industry is making the switch. In the video, Steve walks us through the Gboard hoarding that wrapped the site during the renovation — paired with our PVC-free self-adhesive vinyl — and explains how the combination delivered the finish and durability the job demanded, without the environmental baggage that comes with traditional materials.
Sustainability’s definitely a focus… a holistic approach to upcycle and reuse, and this product delivers that very effectively, very efficiently.
Steve Filear, General Manager, Discus Print & Signage
It’s a story we’re proud to be part of. The hoarding is built with Gboard — part of a closed-loop recycling system that keeps end-of-life material out of landfill and back in circulation — and finished with our PVC-free SAV. And since hoarding comes down once the works wrap up, that closed loop matters: the material, both SAV and Board, get a second life rather than heading to landfill.
For printers and sign makers watching on, Steve’s message is a simple one: the sustainable option is no longer the compromise option. It performs on the wall, it stacks up commercially, and it puts your work on the right side of where the industry is heading.
Watch the full conversation with Steve below.
Want to know more about PVC-free materials, the Visionary Green program, or Gboard? Head straight to our Visionary Green or Gboard page, or email the team at [email protected].
Visionary Knowledge
Published Date: September 2025

One-way window films are an incredible way to transform windows into bold, high-impact advertising or decoration, without losing visibility from the inside. But not all films are created equal — and choosing the right perforation pattern for your project is critical to balancing print quality, visibility, and light transmission.
At Visionary, we offer the largest range of one-way films on the planet, giving you options from 20% perforation for maximum graphic impact through to 50% perforation for vehicle safety and clear visibility.
Perforation refers to the diameter and number of holes in the film. Typically, the more perforation, the more see-through it is — but at the cost of printable surface area. The less perforation, the more space for ink, meaning stronger colours and higher impact graphics, but reduced visibility and light passing through.
Here’s how different options work:
20% Open Area – Maximum Print Impact
30% Open Area – Best of Both Worlds
40% Open Area – The All-Rounder
50% Open Area – King of the Road
Choosing the right film isn’t just about the image you want — it’s also about where and how it’s being used:
Not every project needs the same level of durability — and that’s why Visionary offers one-way films to suit every budget and performance requirement:
Whatever the project, Visionary has a solution that balances performance, longevity, and budget.
At Visionary, we stock the largest range of sizes to ensure your project is never limited by material width. Our MegaView and Innova ranges are available in 1372mm and 1520mm widths as standard, across every perforation pattern.
Need something bigger or more specific? We also supply bespoke options, including 980mm wide films and 250m jumbo rolls — giving you the flexibility to take on projects of any scale with ease.
Visionary is Australia’s trusted source for one-way window films, offering the widest range of options to suit any project. From bold, high-impact retail graphics to compliant vehicle and transit solutions, we provide films that deliver superior print quality, durability, and safety.
With decades of industry experience and a strong focus on innovation, sustainability, and local support, Visionary ensures you get the right product for your needs every time. Our team will guide you in selecting the perfect perforation pattern and material, so your project achieves the ideal balance of impact, visibility, and compliance.
Choosing the right Visionary One Way product is the difference between a safe, compliant, high-performing installation and one that misses the mark. Whether you need eye-popping retail graphics, all-round transport solutions, or maximum visibility for vehicles, Visionary has the perfect product to bring your vision to life.
For tailored advice, get in touch with the Visionary team at visionarydigital.com.au.